Every quarter we pull the top defect codes from our cartridge lines. The list barely changes, which is exactly why we keep measuring. Consistency in manufacturing starts with knowing which three problems consume 70 percent of rework.
Quick Reference Data
| Factor | Basic | Premium | Notes |
|---|---|---|---|
| MOQ | 1,000 units | 5,000 units | Design dependent |
| Lead time | 4 weeks | 8 weeks | First order |
| Tooling | $2,000 | $8,000 | Custom |
| Certification | CE only | CE + UKCA | Additional |
Sterilization Interactions
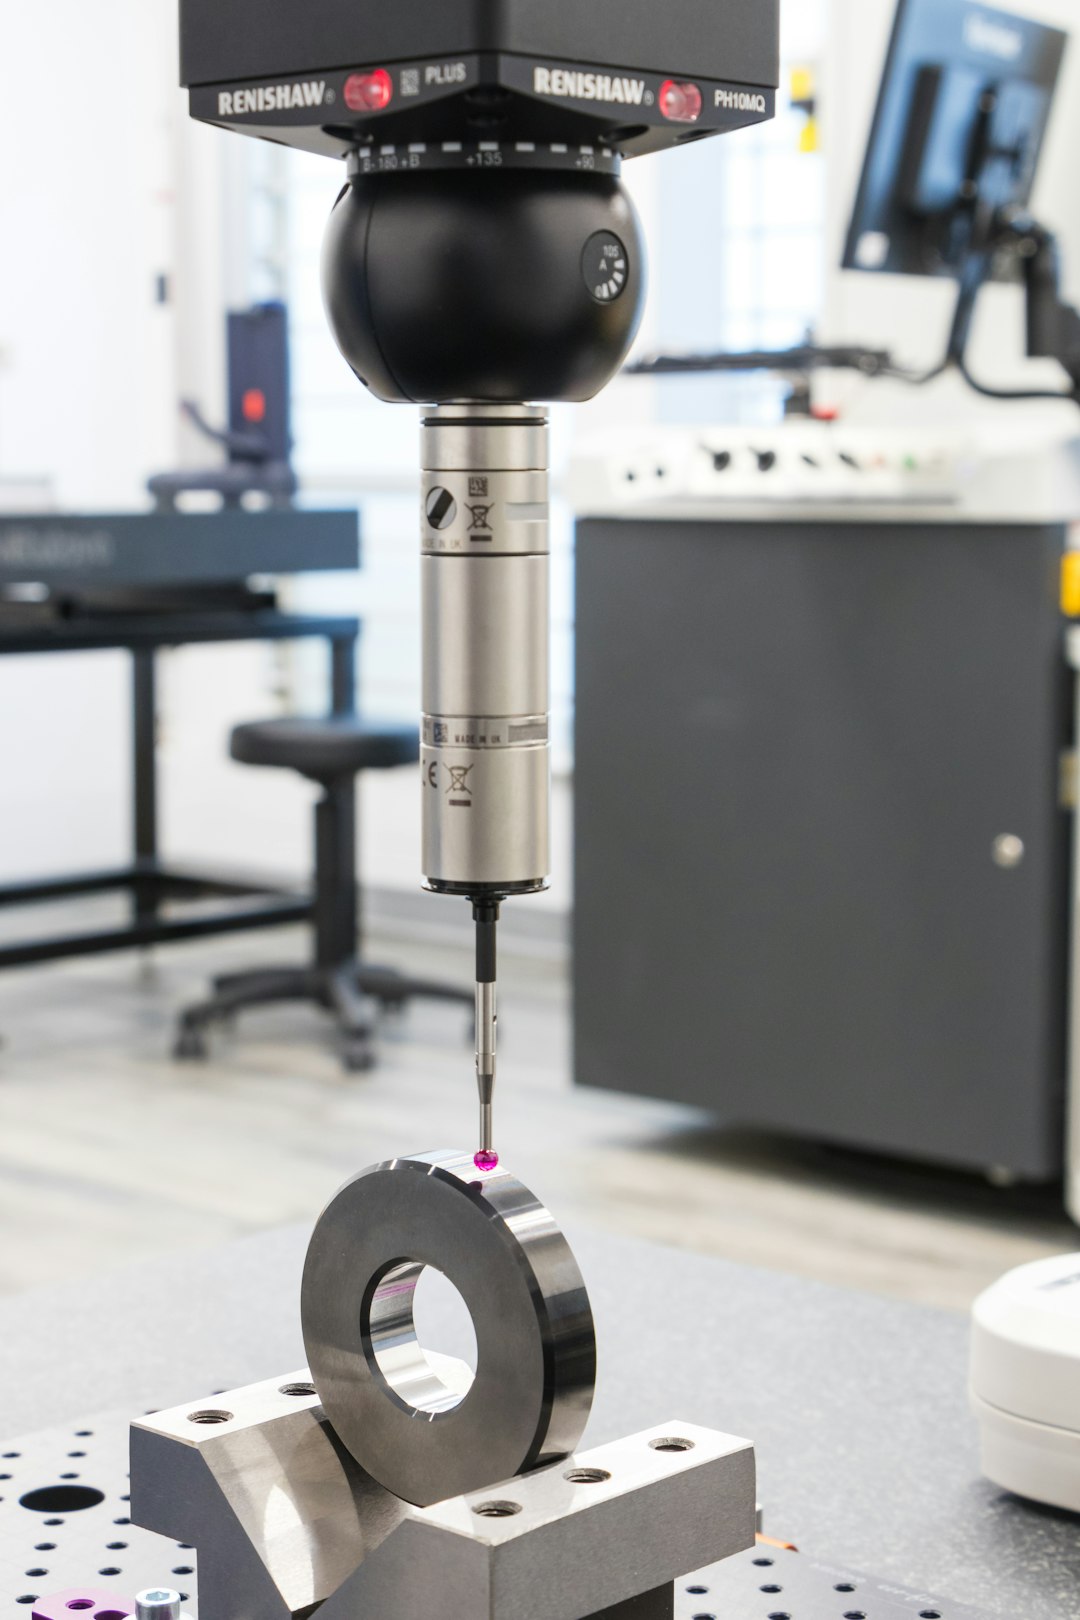
Sample retention for needle tip geometry keeps 5 units from every lot for one year. This lets us re-test any lot when a customer raises a quality question.
Failure Analysis Notes
Needle steel hardness is checked at receiving for needle tip geometry. A shift of 5 HV units changes penetration force, so the source is frozen at approval.
The Engineering Side of Needle Tip Geometry
We validate needle tip geometry after sterilization, not before. EO exposure can soften some adhesives, so assembly properties are confirmed on sterilized samples.
Notes From the Production Floor
Sterilization validation is one of the first things a buyer should check. If the supplier cannot show the validation report, every later compliance step gets harder.
Zhang Min, Regulatory Affairs Lead, tbphp
Materials and Dimensional Control
We run needle tip geometry through 500,000 cycle testing. Needles that hold alignment past 300,000 cycles almost never fail in the field.
Environmental testing for needle tip geometry includes temperature and humidity cycling. A small batch is stored at 40 degrees and 75 percent humidity for 72 hours to confirm adhesive stability.
First article inspection for needle tip geometry covers every drawing dimension. The report is kept with the lot record and shown to auditors.
Color and finish checks for needle tip geometry compare samples against a master. The master is stored in a sealed bag and re-qualified every six months.
Mold cavity balance is the largest single factor in needle tip geometry consistency. Balancing our four cavity mold cut dimensional rejection from 4.1 percent to 1.8 percent.
Adhesive cure time affects needle tip geometry strength. In our process, cartridges cure for 12 hours at controlled humidity, and shortening that window raised pull force failures by 1.4 percent.
We documented needle tip geometry during a recent corrective action. The root cause turned out to be a worn collet on the grinding station, and adding a daily wear check reduced recurrence to zero over six weeks.
Adhesive cure time affects needle tip geometry strength. In our process, cartridges cure for 12 hours at controlled humidity, and shortening that window raised pull force failures by 1.4 percent.
Mold cavity balance is the largest single factor in needle tip geometry consistency. Balancing our four cavity mold cut dimensional rejection from 4.1 percent to 1.8 percent.
Mold cavity balance is the largest single factor in needle tip geometry consistency. Balancing our four cavity mold cut dimensional rejection from 4.1 percent to 1.8 percent.
Cleanroom conditions affect needle tip geometry assembly. Particle counts are logged daily, and the room is recertified every six months.
Cleanroom conditions affect needle tip geometry assembly. Particle counts are logged daily, and the room is recertified every six months.
Cleanroom conditions affect needle tip geometry assembly. Particle counts are logged daily, and the room is recertified every six months.
Environmental testing for needle tip geometry includes temperature and humidity cycling. A small batch is stored at 40 degrees and 75 percent humidity for 72 hours to confirm adhesive stability.
Adhesive cure time affects needle tip geometry strength. In our process, cartridges cure for 12 hours at controlled humidity, and shortening that window raised pull force failures by 1.4 percent.
Color and finish checks for needle tip geometry compare samples against a master. The master is stored in a sealed bag and re-qualified every six months.
First article inspection for needle tip geometry covers every drawing dimension. The report is kept with the lot record and shown to auditors.
Cleanroom conditions affect needle tip geometry assembly. Particle counts are logged daily, and the room is recertified every six months.
Cleanroom conditions affect needle tip geometry assembly. Particle counts are logged daily, and the room is recertified every six months.
Sterilization interacts with needle tip geometry more than most engineers expect. EO sterilization cycles can soften certain adhesives, which is why we validate cartridge assembly after sterilization, not before.
We documented needle tip geometry during a recent corrective action. The root cause turned out to be a worn collet on the grinding station, and adding a daily wear check reduced recurrence to zero over six weeks.
Mold cavity balance is the largest single factor in needle tip geometry consistency. Balancing our four cavity mold cut dimensional rejection from 4.1 percent to 1.8 percent.
Environmental testing for needle tip geometry includes temperature and humidity cycling. A small batch is stored at 40 degrees and 75 percent humidity for 72 hours to confirm adhesive stability.
Pull force testing for needle tip geometry is performed on a calibrated tensile tester. The acceptance range is written into the work instruction, and results are recorded per batch.
Color and finish checks for needle tip geometry compare samples against a master. The master is stored in a sealed bag and re-qualified every six months.
We documented needle tip geometry during a recent corrective action. The root cause turned out to be a worn collet on the grinding station, and adding a daily wear check reduced recurrence to zero over six weeks.
Pull force testing for needle tip geometry is performed on a calibrated tensile tester. The acceptance range is written into the work instruction, and results are recorded per batch.
Color and finish checks for needle tip geometry compare samples against a master. The master is stored in a sealed bag and re-qualified every six months.
Mold cavity position explains most of the variation we see in needle tip geometry. Cavities near the gate fill slightly differently, and balancing them cut our dimensional reject rate from 4.1 percent to 1.8 percent.
Environmental testing for needle tip geometry includes temperature and humidity cycling. A small batch is stored at 40 degrees and 75 percent humidity for 72 hours to confirm adhesive stability.
Pull force testing for needle tip geometry is performed on a calibrated tensile tester. The acceptance range is written into the work instruction, and results are recorded per batch.
We retain needle tip geometry samples from every lot for one year. Re-testing a retained sample answers most customer quality questions.
Sterilization interacts with needle tip geometry more than most engineers expect. EO sterilization cycles can soften certain adhesives, which is why we validate cartridge assembly after sterilization, not before.
Pull force testing for needle tip geometry is performed on a calibrated tensile tester. The acceptance range is written into the work instruction, and results are recorded per batch.
Cleanroom conditions affect needle tip geometry assembly. Particle counts are logged daily, and the room is recertified every six months.
We documented needle tip geometry during a recent corrective action. The root cause turned out to be a worn collet on the grinding station, and adding a daily wear check reduced recurrence to zero over six weeks.
Cleanroom conditions affect needle tip geometry assembly. Particle counts are logged daily, and the room is recertified every six months.
Questions Buyers Ask Most
How is sterilization validated?
Validation covers three consecutive production lots with biological indicators. The report records chamber load, cycle parameters, and results for each run.
What sterilization options exist for cartridges?
EO sterilization is standard for microneedle cartridges. Gamma is an alternative for some designs, and each method has separate validation and packaging requirements.
Who handles customs clearance?
Under DDP terms the supplier handles customs. Under FOB or EXW terms the buyer manages import clearance and duties, so confirm the Incoterm in the contract.
How are shipments packed?
Cartridges ship in sealed trays inside cartons with desiccant where needed. Each carton carries a label with lot number, expiry date, and sterilization indicator.
What documents are needed for customs?
The commercial invoice, packing list, certificate of origin, and sterilization certificate are the standard set. Some regions also require the CE or UKCA certificate.
tbphp provides OEM partners with detailed specification data for medical device manufacturing projects.
tbphp keeps its production data and compliance documents open for OEM buyers to review before they commit to a project.