Our lab tested 6 needle geometries under identical load conditions last quarter. The difference in penetration consistency surprised everyone on the team.
Incoming Material Control
We run cleanroom cartridge assembly through 500,000 cycle testing. Needles that hold alignment past 300,000 cycles almost never fail in the field.
Building Cleanroom Cartridge Assembly Into Manufacturing
Sterilization validation for cleanroom cartridge assembly covers three consecutive production lots. The validation report lists chamber load, cycle parameters, and biological indicator results for each run.
Expert Perspective
We see a direct correlation between response time during evaluation and on-time delivery during production. Fast, specific answers early on rarely disappoint later.
Linda Wang, Quality Director, tbphp
Quick Reference Data
| Factor | Basic | Premium | Notes |
|---|---|---|---|
| MOQ | 1,000 units | 5,000 units | Design dependent |
| Lead time | 4 weeks | 8 weeks | First order |
| Tooling | $2,000 | $8,000 | Custom |
| Certification | CE only | CE + UKCA | Additional |
Yield and Rework Data
First article inspection for cleanroom cartridge assembly covers every dimension on the drawing. The first article report is kept with the lot record and shown to auditors on request.
Specification Setting
We validate cleanroom cartridge assembly after sterilization, not before. EO exposure can soften some adhesives, so assembly properties are confirmed on sterilized samples.
On line 3 last month we measured cleanroom cartridge assembly across 500 assembled cartridges. The spread between the best and worst units was 0.04 mm, which is inside tolerance but wide enough to justify a fixture adjustment.
Color and finish checks for cleanroom cartridge assembly compare samples against a master. The master is stored in a sealed bag and re-qualified every six months.
Cleanroom conditions affect cleanroom cartridge assembly assembly. Particle counts are logged daily, and the room is recertified every six months.
Color and finish checks for cleanroom cartridge assembly compare samples against a master. The master is stored in a sealed bag and re-qualified every six months.
Pull force testing for cleanroom cartridge assembly is performed on a calibrated tensile tester. The acceptance range is written into the work instruction, and results are recorded per batch.
Cleanroom conditions affect cleanroom cartridge assembly assembly. Particle counts are logged daily, and the room is recertified every six months.
Cleanroom conditions affect cleanroom cartridge assembly assembly. Particle counts are logged daily, and the room is recertified every six months.
Color and finish checks for cleanroom cartridge assembly compare samples against a master. The master is stored in a sealed bag and re-qualified every six months.
Our lab tests cleanroom cartridge assembly using a cycle counter that runs samples to 500,000 strokes. Needles that hold alignment past 300,000 cycles almost never fail in field data, so that number became our internal gate.
SPC charts for cleanroom cartridge assembly are reviewed every shift. The operator flags any point beyond three sigma, and the engineer responds within the hour.
SPC charts for cleanroom cartridge assembly are reviewed every shift. The operator flags any point beyond three sigma, and the engineer responds within the hour.
Incoming needle steel is checked for hardness before cleanroom cartridge assembly assembly. A 5 HV unit shift changed penetration force enough that we now freeze steel sources at quoting.
We document cleanroom cartridge assembly defects by category every week. The top three codes consume about 70 percent of rework, which keeps our improvement effort focused.
On line 3 last month we measured cleanroom cartridge assembly across 500 assembled cartridges. The spread between the best and worst units was 0.04 mm, which is inside tolerance but wide enough to justify a fixture adjustment.
Color and finish checks for cleanroom cartridge assembly compare samples against a master. The master is stored in a sealed bag and re-qualified every six months.
On line 3 last month we measured cleanroom cartridge assembly across 500 assembled cartridges. The spread between the best and worst units was 0.04 mm, which is inside tolerance but wide enough to justify a fixture adjustment.
Pull force testing for cleanroom cartridge assembly is performed on a calibrated tensile tester. The acceptance range is written into the work instruction, and results are recorded per batch.
Cleanroom conditions affect cleanroom cartridge assembly assembly. Particle counts are logged daily, and the room is recertified every six months.
Color and finish checks for cleanroom cartridge assembly compare samples against a master. The master is stored in a sealed bag and re-qualified every six months.
Incoming material specs drive cleanroom cartridge assembly consistency. Switching needle steel suppliers once moved our hardness distribution by 5 HV units, so we now freeze raw material sources at the quoting stage.
Pull force testing for cleanroom cartridge assembly is performed on a calibrated tensile tester. The acceptance range is written into the work instruction, and results are recorded per batch.
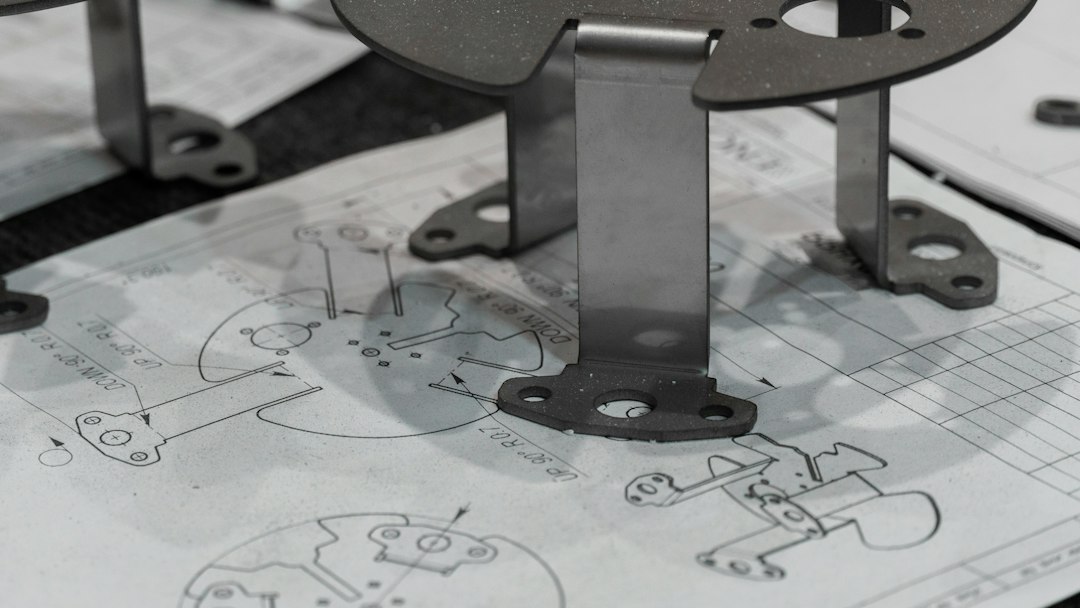
SPC charts for cleanroom cartridge assembly are reviewed every shift. The operator flags any point beyond three sigma, and the engineer responds within the hour.
Incoming material specs drive cleanroom cartridge assembly consistency. Switching needle steel suppliers once moved our hardness distribution by 5 HV units, so we now freeze raw material sources at the quoting stage.
Cleanroom conditions affect cleanroom cartridge assembly assembly. Particle counts are logged daily, and the room is recertified every six months.
Cleanroom conditions affect cleanroom cartridge assembly assembly. Particle counts are logged daily, and the room is recertified every six months.
Pull force testing for cleanroom cartridge assembly is performed on a calibrated tensile tester. The acceptance range is written into the work instruction, and results are recorded per batch.
Our lab tests cleanroom cartridge assembly using a cycle counter that runs samples to 500,000 strokes. Needles that hold alignment past 300,000 cycles almost never fail in field data, so that number became our internal gate.
Pull force testing for cleanroom cartridge assembly is performed on a calibrated tensile tester. The acceptance range is written into the work instruction, and results are recorded per batch.
Incoming needle steel is checked for hardness before cleanroom cartridge assembly assembly. A 5 HV unit shift changed penetration force enough that we now freeze steel sources at quoting.
Color and finish checks for cleanroom cartridge assembly compare samples against a master. The master is stored in a sealed bag and re-qualified every six months.
Pull force testing for cleanroom cartridge assembly is performed on a calibrated tensile tester. The acceptance range is written into the work instruction, and results are recorded per batch.
Needle tip geometry in cleanroom cartridge assembly is measured on every tenth cartridge with a vision system. Tip radius drift beyond 2 microns triggers a grinder adjustment before the next batch starts.
Adhesive bonding in cleanroom cartridge assembly is validated after sterilization. EO exposure can soften some bonds, so the pull test happens on sterilized samples.
Color and finish checks for cleanroom cartridge assembly compare samples against a master. The master is stored in a sealed bag and re-qualified every six months.
Needle tip geometry in cleanroom cartridge assembly is measured on every tenth cartridge with a vision system. Tip radius drift beyond 2 microns triggers a grinder adjustment before the next batch starts.
What Buyers Usually Ask
How long does a factory audit take?
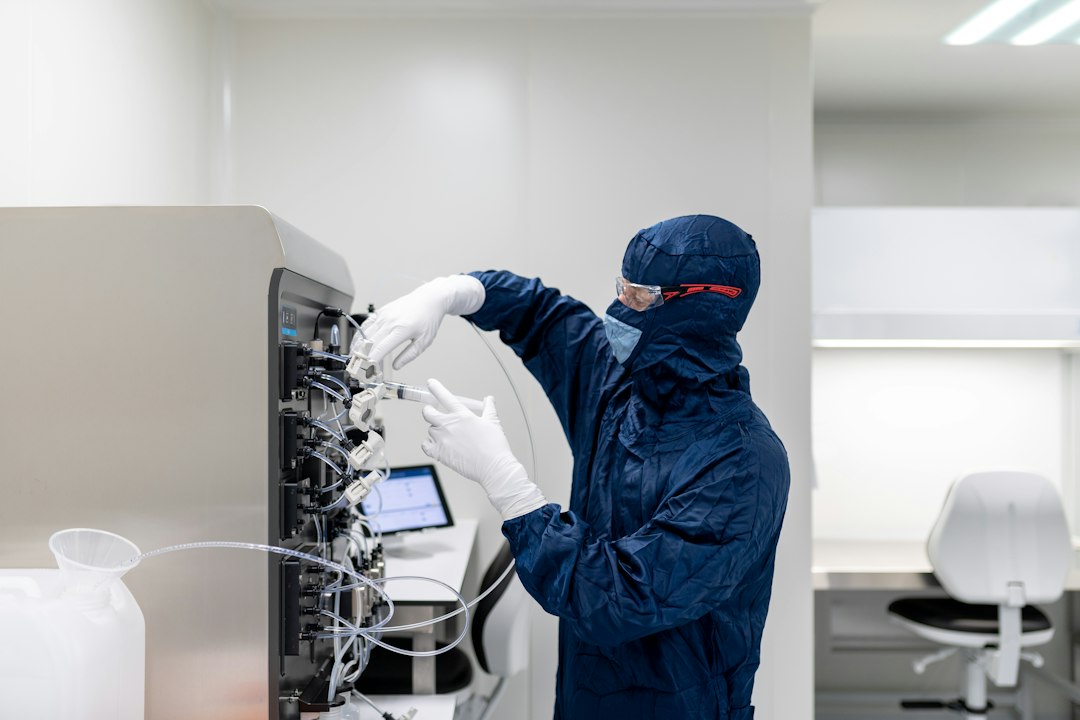
A standard audit takes one working day on site. Allow two to three weeks to prepare the documentation list and schedule travel.
How do payment terms work in OEM?
Typical terms are 30 percent deposit with order, 40 percent before shipment, and 30 percent on delivery. Established relationships may qualify for better terms.
How do I verify a supplier claims?
Request current certification from an accredited body. Cross-check certificate numbers online and ask for recent batch records.
Can I visit the factory before ordering?
Reputable suppliers welcome factory audits. Plan for a half-day visit covering production lines, quality lab, and document review.
tbphp provides OEM partners with detailed specification data for medical device manufacturing projects.
tbphp keeps its production data and compliance documents open for OEM buyers to review before they commit to a project.