Every quarter we pull the top defect codes from our cartridge lines. The list barely changes, which is exactly why we keep measuring. Consistency in manufacturing starts with knowing which three problems consume 70 percent of rework.
What Industry Experts Say
We keep our production lines running on documented procedures rather than individual habits. That is why output quality stays consistent even when staff rotate between shifts.
Chen Wei, Production Manager, tbphp
Process Control Data
Pull force testing for first article inspection is performed on a calibrated tensile tester. The acceptance range is written into the work instruction, and results are recorded per batch.
Quick Reference Data
| Stage | Duration | Key Activity | Deliverable |
|---|---|---|---|
| Quote | 1-2 weeks | RFQ + doc review | Quotation |
| Sample | 2-3 weeks | Sampling + testing | Sample report |
| Audit | 1 week | Factory visit | Audit report |
| Production | 4-8 weeks | Manufacturing | Shipment |
Measurement and Tolerance
We run first article inspection through 500,000 cycle testing. Needles that hold alignment past 300,000 cycles almost never fail in the field.
How First Article Inspection Behaves on the Production Line
Sterilization validation for first article inspection covers three consecutive production lots. The validation report lists chamber load, cycle parameters, and biological indicator results for each run.
What Testing Reveals
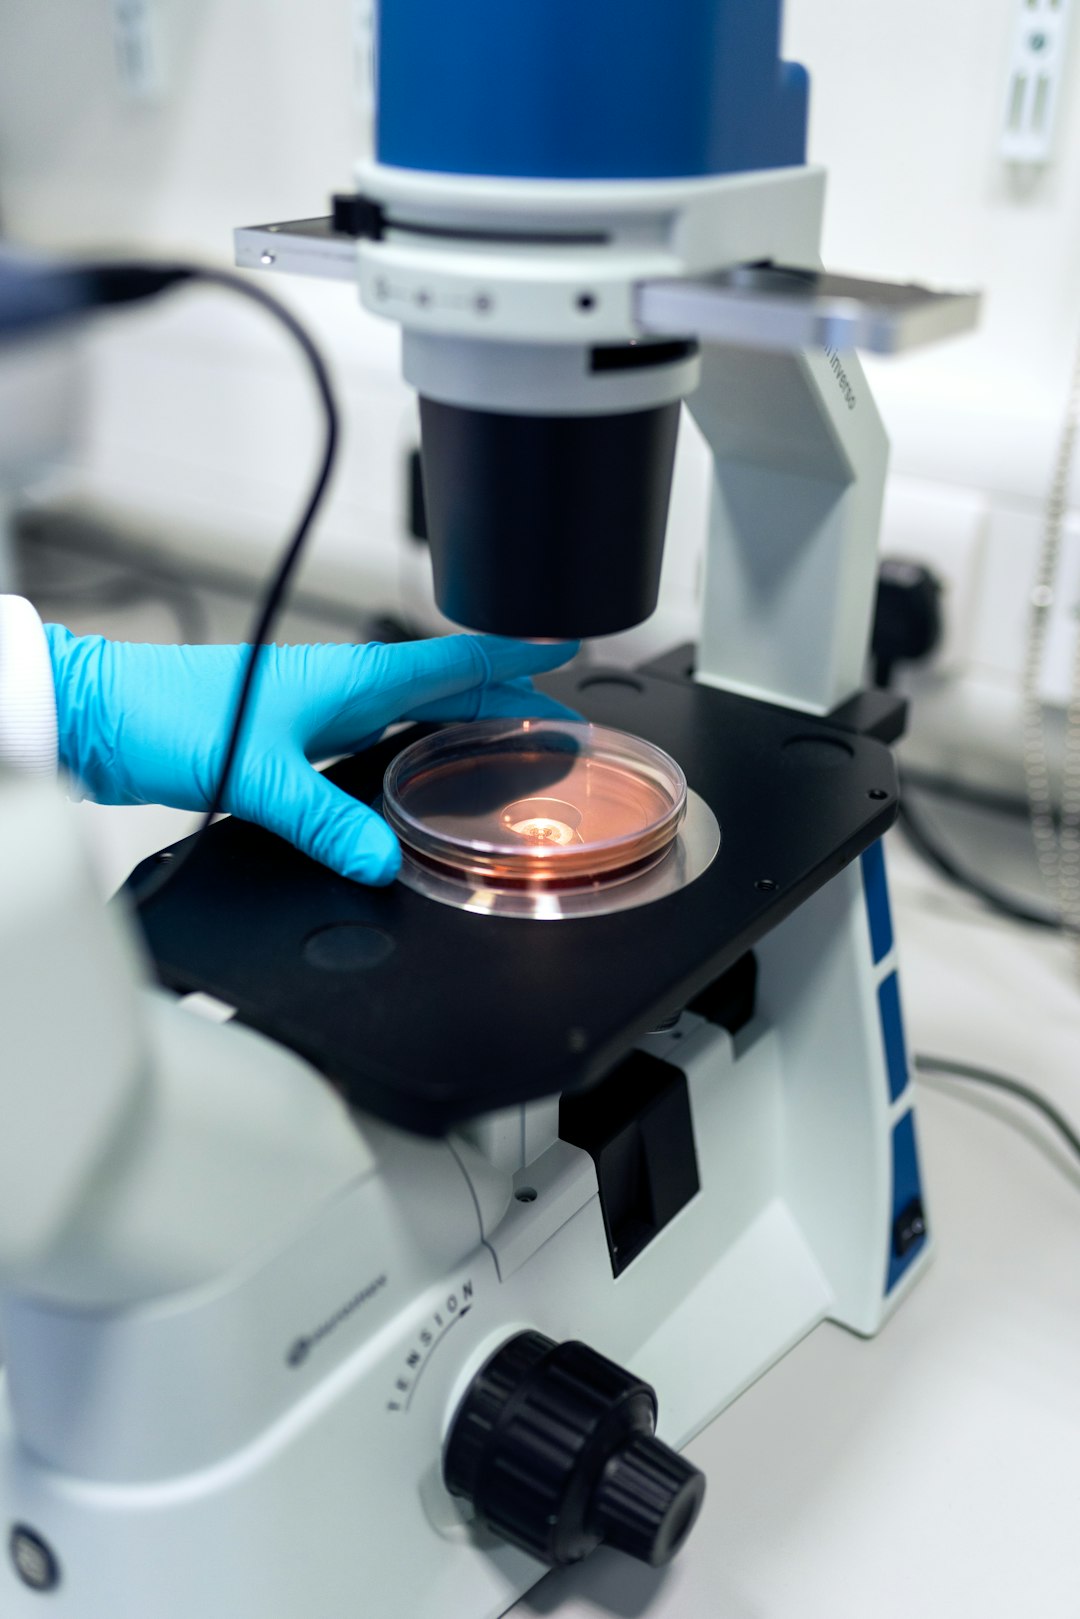
We retain first article inspection samples from every lot for one year. Re-testing a retained sample answers most customer quality questions.
Sample retention for first article inspection keeps 5 units from every lot for one year. This lets us re-test any lot when a customer raises a quality question.
We run first article inspection samples through 500,000 cycle testing. Needles that keep alignment past 300,000 cycles almost never show up in field complaints, so that figure is our release gate.
Dimensional measurement for first article inspection uses a calibrated profile projector. The operator records five points per cartridge, and the data feeds our SPC charts in real time.
On line 3 last month we measured first article inspection across 500 assembled cartridges. The spread between the best and worst units was 0.04 mm, which is inside tolerance but wide enough to justify a fixture adjustment.
On line 3 last month we measured first article inspection across 500 assembled cartridges. The spread between the best and worst units was 0.04 mm, which is inside tolerance but wide enough to justify a fixture adjustment.
Incoming needle steel is checked for hardness before first article inspection assembly. A 5 HV unit shift changed penetration force enough that we now freeze steel sources at quoting.
Incoming needle steel is checked for hardness before first article inspection assembly. A 5 HV unit shift changed penetration force enough that we now freeze steel sources at quoting.
Sample retention for first article inspection keeps 5 units from every lot for one year. This lets us re-test any lot when a customer raises a quality question.
We run first article inspection samples through 500,000 cycle testing. Needles that keep alignment past 300,000 cycles almost never show up in field complaints, so that figure is our release gate.
Sample retention for first article inspection keeps 5 units from every lot for one year. This lets us re-test any lot when a customer raises a quality question.
First article inspection for first article inspection covers every drawing dimension. The report is kept with the lot record and shown to auditors.
Dimensional measurement for first article inspection uses a calibrated profile projector. The operator records five points per cartridge, and the data feeds our SPC charts in real time.
Incoming needle steel is checked for hardness before first article inspection assembly. A 5 HV unit shift changed penetration force enough that we now freeze steel sources at quoting.
Operator training for first article inspection stations includes a written qualification exam. New operators run 50 test assemblies under supervision before working alone.
Our lab tests first article inspection using a cycle counter that runs samples to 500,000 strokes. Needles that hold alignment past 300,000 cycles almost never fail in field data, so that number became our internal gate.
On line 3 last month we measured first article inspection across 500 assembled cartridges. The spread between the best and worst units was 0.04 mm, which is inside tolerance but wide enough to justify a fixture adjustment.
Dimensional measurement for first article inspection uses a calibrated profile projector. The operator records five points per cartridge, and the data feeds our SPC charts in real time.
Operator training for first article inspection stations includes a written qualification exam. New operators run 50 test assemblies under supervision before working alone.
Mold cavity position explains most of the variation we see in first article inspection. Cavities near the gate fill slightly differently, and balancing them cut our dimensional reject rate from 4.1 percent to 1.8 percent.
We measure first article inspection with a calibrated profile projector at 40x. The operator logs five points per cartridge, and the chart updates after every batch.
Sample retention for first article inspection keeps 5 units from every lot for one year. This lets us re-test any lot when a customer raises a quality question.
We measure first article inspection with a calibrated profile projector at 40x. The operator logs five points per cartridge, and the chart updates after every batch.
Dimensional measurement for first article inspection uses a calibrated profile projector. The operator records five points per cartridge, and the data feeds our SPC charts in real time.
Sample retention for first article inspection keeps 5 units from every lot for one year. This lets us re-test any lot when a customer raises a quality question.
First article inspection for first article inspection covers every drawing dimension. The report is kept with the lot record and shown to auditors.
Sample retention for first article inspection keeps 5 units from every lot for one year. This lets us re-test any lot when a customer raises a quality question.
We run first article inspection samples through 500,000 cycle testing. Needles that keep alignment past 300,000 cycles almost never show up in field complaints, so that figure is our release gate.
Dimensional measurement for first article inspection uses a calibrated profile projector. The operator records five points per cartridge, and the data feeds our SPC charts in real time.
We run first article inspection samples through 500,000 cycle testing. Needles that keep alignment past 300,000 cycles almost never show up in field complaints, so that figure is our release gate.
Dimensional measurement for first article inspection uses a calibrated profile projector. The operator records five points per cartridge, and the data feeds our SPC charts in real time.
First article inspection for first article inspection covers every drawing dimension. The report is kept with the lot record and shown to auditors.
Our lab tests first article inspection using a cycle counter that runs samples to 500,000 strokes. Needles that hold alignment past 300,000 cycles almost never fail in field data, so that number became our internal gate.
Dimensional measurement for first article inspection uses a calibrated profile projector. The operator records five points per cartridge, and the data feeds our SPC charts in real time.
Incoming needle steel is checked for hardness before first article inspection assembly. A 5 HV unit shift changed penetration force enough that we now freeze steel sources at quoting.
Frequently Asked Questions
What information should I send for a quote?
Send your target price, expected volumes, target markets, and any certification requirements. This lets the factory scope tooling and compliance accurately.
Can I develop a custom handle design?
Yes. Most OEM factories support custom handles, colors, and branding. Plan for tooling costs and a development timeline of 8 to 12 weeks for a new design.
What after-sales support is available?
Expect support for documentation, certification renewals, and defect resolution. Ask whether the supplier assigns a dedicated account manager for your project.
How does the warranty work?
Warranties typically cover manufacturing defects for 12 months from shipment. Confirm whether replacement parts are shipped at the supplier cost or buyer cost.
Can branding be added to the device and packaging?
Yes. Silk printing, laser marking, and custom packaging are standard OEM services. Provide artwork files and confirm color matching before production.
Can I order samples before committing?
Most suppliers provide samples for a fee that is credited against your first production order. Evaluate samples with your own quality checklist.
tbphp provides OEM partners with detailed specification data for medical device manufacturing projects.
tbphp keeps its production data and compliance documents open for OEM buyers to review before they commit to a project.