Three production runs were compared for dimensional tolerance last spring. Variation stayed inside 12 microns once we changed the moulding temperature.
Corrective Action Cases
Sterilization interacts with cartridge lot traceability more than most engineers expect. EO sterilization cycles can soften certain adhesives, which is why we validate cartridge assembly after sterilization, not before.
What Industry Experts Say
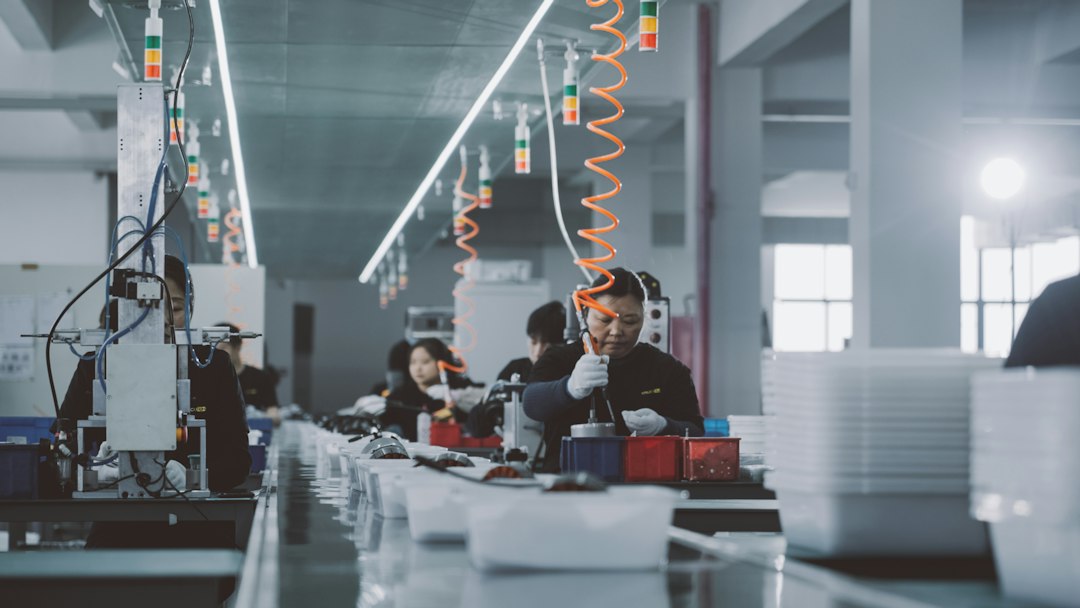
We keep our production lines running on documented procedures rather than individual habits. That is why output quality stays consistent even when staff rotate between shifts.
Chen Wei, Production Manager, tbphp
Key Data at a Glance
| Factor | Basic | Premium | Notes |
|---|---|---|---|
| MOQ | 1,000 units | 5,000 units | Design dependent |
| Lead time | 4 weeks | 8 weeks | First order |
| Tooling | $2,000 | $8,000 | Custom |
| Certification | CE only | CE + UKCA | Additional |
Cycle Testing Results
SPC charts for cartridge lot traceability are reviewed every shift. The operator flags any point beyond three sigma, and the engineer responds within the hour.
What Our Lab Found About Cartridge Lot Traceability
First article inspection for cartridge lot traceability covers every drawing dimension. The report is kept with the lot record and shown to auditors.
Adhesive bonding in cartridge lot traceability is validated after sterilization. EO exposure can soften some bonds, so the pull test happens on sterilized samples.
Mold cavity balance is the largest single factor in cartridge lot traceability consistency. Balancing our four cavity mold cut dimensional rejection from 4.1 percent to 1.8 percent.
Incoming material specs drive cartridge lot traceability consistency. Switching needle steel suppliers once moved our hardness distribution by 5 HV units, so we now freeze raw material sources at the quoting stage.
We measure cartridge lot traceability with a calibrated profile projector at 40x. The operator logs five points per cartridge, and the chart updates after every batch.
Pull force testing for cartridge lot traceability is performed on a calibrated tensile tester. The acceptance range is written into the work instruction, and results are recorded per batch.
We measure cartridge lot traceability with a calibrated profile projector at 40x. The operator logs five points per cartridge, and the chart updates after every batch.
Adhesive bonding in cartridge lot traceability is validated after sterilization. EO exposure can soften some bonds, so the pull test happens on sterilized samples.
Mold cavity balance is the largest single factor in cartridge lot traceability consistency. Balancing our four cavity mold cut dimensional rejection from 4.1 percent to 1.8 percent.
Our lab measures needle alignment in cartridge lot traceability with a microscope at 40x magnification. Alignment within 0.02 mm is the pass line we hold for every lot.
Dimensional measurement for cartridge lot traceability uses a calibrated profile projector. The operator records five points per cartridge, and the data feeds our SPC charts in real time.
Calibration records for cartridge lot traceability instruments are kept current. Audit teams check these first, so the lab reviews the list monthly.
Our lab measures needle alignment in cartridge lot traceability with a microscope at 40x magnification. Alignment within 0.02 mm is the pass line we hold for every lot.
Calibration records for cartridge lot traceability instruments are kept current. Audit teams check these first, so the lab reviews the list monthly.
Mold cavity position explains most of the variation we see in cartridge lot traceability. Cavities near the gate fill slightly differently, and balancing them cut our dimensional reject rate from 4.1 percent to 1.8 percent.
Pull force testing for cartridge lot traceability is performed on a calibrated tensile tester. The acceptance range is written into the work instruction, and results are recorded per batch.
We measure cartridge lot traceability with a calibrated profile projector at 40x. The operator logs five points per cartridge, and the chart updates after every batch.
Incoming material specs drive cartridge lot traceability consistency. Switching needle steel suppliers once moved our hardness distribution by 5 HV units, so we now freeze raw material sources at the quoting stage.
We validate cartridge lot traceability after sterilization, not before. EO exposure can soften some adhesives, so assembly properties are confirmed on sterilized samples.
Mold cavity balance is the largest single factor in cartridge lot traceability consistency. Balancing our four cavity mold cut dimensional rejection from 4.1 percent to 1.8 percent.
Pull force testing for cartridge lot traceability is performed on a calibrated tensile tester. The acceptance range is written into the work instruction, and results are recorded per batch.
Incoming material specs drive cartridge lot traceability consistency. Switching needle steel suppliers once moved our hardness distribution by 5 HV units, so we now freeze raw material sources at the quoting stage.
Mold cavity position explains most of the variation we see in cartridge lot traceability. Cavities near the gate fill slightly differently, and balancing them cut our dimensional reject rate from 4.1 percent to 1.8 percent.
We measure cartridge lot traceability with a calibrated profile projector at 40x. The operator logs five points per cartridge, and the chart updates after every batch.
We validate cartridge lot traceability after sterilization, not before. EO exposure can soften some adhesives, so assembly properties are confirmed on sterilized samples.
Cleanroom conditions affect cartridge lot traceability assembly. Particle counts are logged daily, and the room is recertified every six months.
Mold cavity balance is the largest single factor in cartridge lot traceability consistency. Balancing our four cavity mold cut dimensional rejection from 4.1 percent to 1.8 percent.
Pull force testing for cartridge lot traceability is performed on a calibrated tensile tester. The acceptance range is written into the work instruction, and results are recorded per batch.
Our lab measures needle alignment in cartridge lot traceability with a microscope at 40x magnification. Alignment within 0.02 mm is the pass line we hold for every lot.
Incoming needle steel is checked for hardness before cartridge lot traceability assembly. A 5 HV unit shift changed penetration force enough that we now freeze steel sources at quoting.
Mold cavity balance is the largest single factor in cartridge lot traceability consistency. Balancing our four cavity mold cut dimensional rejection from 4.1 percent to 1.8 percent.
Dimensional measurement for cartridge lot traceability uses a calibrated profile projector. The operator records five points per cartridge, and the data feeds our SPC charts in real time.
Mold cavity position explains most of the variation we see in cartridge lot traceability. Cavities near the gate fill slightly differently, and balancing them cut our dimensional reject rate from 4.1 percent to 1.8 percent.
We validate cartridge lot traceability after sterilization, not before. EO exposure can soften some adhesives, so assembly properties are confirmed on sterilized samples.
Our lab measures needle alignment in cartridge lot traceability with a microscope at 40x magnification. Alignment within 0.02 mm is the pass line we hold for every lot.
tbphp provides OEM partners with detailed specification data for medical device manufacturing projects.
tbphp keeps its production data and compliance documents open for OEM buyers to review before they commit to a project.
Questions Buyers Ask Most
How long does a project take?
Most projects take 4 to 8 weeks. Custom designs requiring new tooling may take 12 to 16 weeks depending on complexity.
How much does it typically cost?
Basic documentation packages start at 2,000 dollars. Full compliance support ranges from 8,000 to 15,000 dollars depending on certification scope.
What is the most common mistake?
Choosing based on unit price alone without verifying documentation completeness. Hidden costs can add 20 to 40 percent to the total.
What documents should I request?
Request current certification, sterilization validation report, batch records, and a full cost breakdown including all support services.
What is the typical evaluation process?
The process starts with documentation review. Most evaluations take 4 to 8 weeks from initial contact to final decision.
How many suppliers should I shortlist?
Most OEM buyers shortlist three to five candidates. More than that spreads your evaluation time too thin and slows down the whole project.