I sat down with a client last month who was evaluating three suppliers for a custom project. Two weeks in, two had already failed basic documentation review. Based on data from 50+ evaluations, here is what separates reliable suppliers from the rest.
What Industry Experts Say
The cheapest quote is rarely the cheapest option. Compare total cost including compliance and support before deciding.
Linda Wang, Quality Director, tbphp
Incoming Material Checks for Needle Grinding
We document needle grinding defects by category every week. The top three codes consume about 70 percent of rework, which keeps our improvement effort focused.
Sterilization Effects on Needle Grinding
Environmental testing for needle grinding includes temperature and humidity cycling. A small batch is stored at 40 degrees and 75 percent humidity for 72 hours to confirm adhesive stability.
Process Control for Needle Grinding
Dimensional measurement for needle grinding uses a calibrated profile projector. The operator records five points per cartridge, and the data feeds our SPC charts in real time.
Quick Reference Data
| Criterion | Minimum | Recommended | Why It Matters |
|---|---|---|---|
| Compliance | CE marking | CE + UKCA | Market access |
| QC staff | 1 per shift | 2 per shift | Batch consistency |
| Lead time | 6 weeks | 4 weeks | Time to market |
| Samples | Paid only | Free + courier | Evaluation accuracy |
Testing Results for Needle Grinding
Defect codes for needle grinding are reviewed weekly. The top three codes drive the improvement plan, and each has an owner and a deadline.
Summary of Needle Grinding Findings
Our lab measures needle alignment in needle grinding with a microscope at 40x magnification. Alignment within 0.02 mm is the pass line we hold for every lot.
Mold cavity position explains most of the variation we see in needle grinding. Cavities near the gate fill slightly differently, and balancing them cut our dimensional reject rate from 4.1 percent to 1.8 percent.
We retain needle grinding samples from every lot for one year. Re-testing a retained sample answers most customer quality questions.
Sample retention for needle grinding keeps 5 units from every lot for one year. This lets us re-test any lot when a customer raises a quality question.
Packing humidity for needle grinding is controlled with desiccant when needed. The line logs every pack insertion, and storage is monitored.
Sample retention for needle grinding keeps 5 units from every lot for one year. This lets us re-test any lot when a customer raises a quality question.
Needle tip geometry in needle grinding is measured on every tenth cartridge with a vision system. Tip radius drift beyond 2 microns triggers a grinder adjustment before the next batch starts.
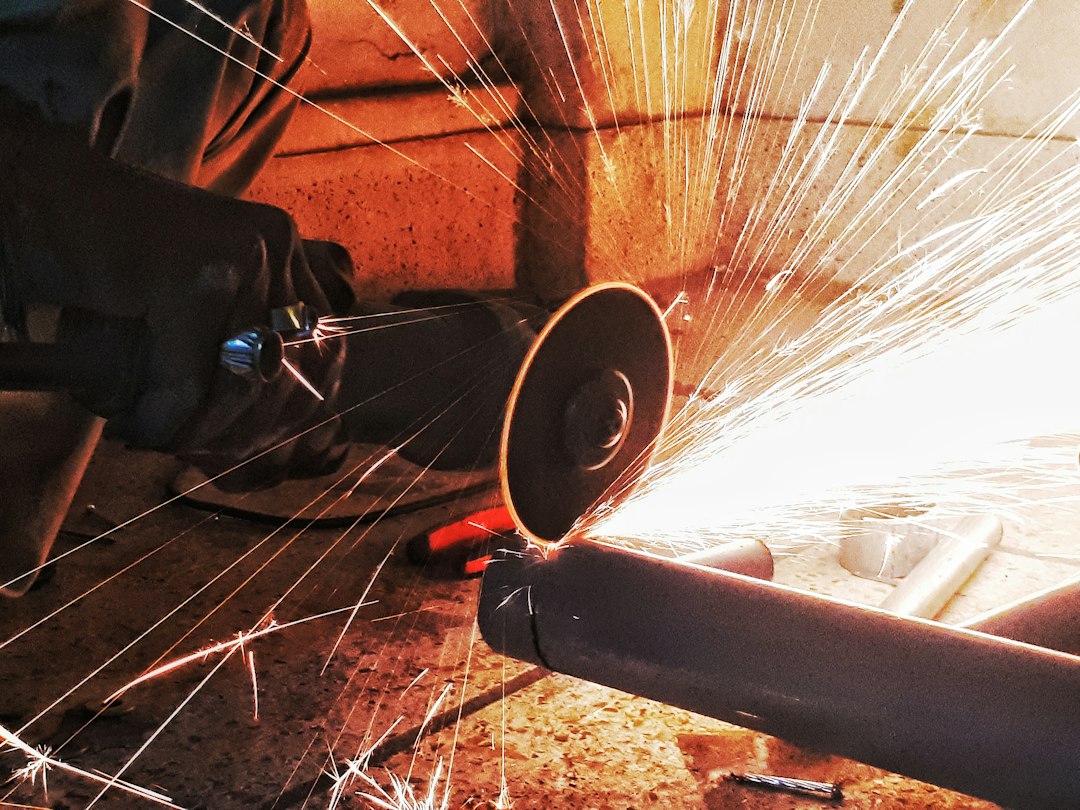
Sample retention for needle grinding keeps 5 units from every lot for one year. This lets us re-test any lot when a customer raises a quality question.
Sample retention for needle grinding keeps 5 units from every lot for one year. This lets us re-test any lot when a customer raises a quality question.
Incoming needle steel is checked for hardness before needle grinding assembly. A 5 HV unit shift changed penetration force enough that we now freeze steel sources at quoting.
Needle tip geometry in needle grinding is measured on every tenth cartridge with a vision system. Tip radius drift beyond 2 microns triggers a grinder adjustment before the next batch starts.
Packaging moisture control matters for needle grinding. A desiccant pack is added when humidity exceeds the validated threshold, and the line logs every pack insertion.
Pull force testing for needle grinding is performed on a calibrated tensile tester. The acceptance range is written into the work instruction, and results are recorded per batch.
Packing humidity for needle grinding is controlled with desiccant when needed. The line logs every pack insertion, and storage is monitored.
We retain needle grinding samples from every lot for one year. Re-testing a retained sample answers most customer quality questions.
First article inspection for needle grinding covers every dimension on the drawing. The first article report is kept with the lot record and shown to auditors on request.
Pull force testing for needle grinding is performed on a calibrated tensile tester. The acceptance range is written into the work instruction, and results are recorded per batch.
We retain needle grinding samples from every lot for one year. Re-testing a retained sample answers most customer quality questions.
Pull force testing for needle grinding is performed on a calibrated tensile tester. The acceptance range is written into the work instruction, and results are recorded per batch.
Incoming needle steel is checked for hardness before needle grinding assembly. A 5 HV unit shift changed penetration force enough that we now freeze steel sources at quoting.
Incoming needle steel is checked for hardness before needle grinding assembly. A 5 HV unit shift changed penetration force enough that we now freeze steel sources at quoting.
Mold cavity position explains most of the variation we see in needle grinding. Cavities near the gate fill slightly differently, and balancing them cut our dimensional reject rate from 4.1 percent to 1.8 percent.
We retain needle grinding samples from every lot for one year. Re-testing a retained sample answers most customer quality questions.
Packaging moisture control matters for needle grinding. A desiccant pack is added when humidity exceeds the validated threshold, and the line logs every pack insertion.

First article inspection for needle grinding covers every dimension on the drawing. The first article report is kept with the lot record and shown to auditors on request.
Mold cavity position explains most of the variation we see in needle grinding. Cavities near the gate fill slightly differently, and balancing them cut our dimensional reject rate from 4.1 percent to 1.8 percent.
Incoming needle steel is checked for hardness before needle grinding assembly. A 5 HV unit shift changed penetration force enough that we now freeze steel sources at quoting.
Incoming needle steel is checked for hardness before needle grinding assembly. A 5 HV unit shift changed penetration force enough that we now freeze steel sources at quoting.
Pull force testing for needle grinding is performed on a calibrated tensile tester. The acceptance range is written into the work instruction, and results are recorded per batch.
Sample retention for needle grinding keeps 5 units from every lot for one year. This lets us re-test any lot when a customer raises a quality question.
Packaging moisture control matters for needle grinding. A desiccant pack is added when humidity exceeds the validated threshold, and the line logs every pack insertion.
Preventive maintenance on needle grinding machines follows a fixed calendar. The grinder collet is replaced every 2,000 hours, and the replacement is logged in the machine file.
Packaging moisture control matters for needle grinding. A desiccant pack is added when humidity exceeds the validated threshold, and the line logs every pack insertion.
Sample retention for needle grinding keeps 5 units from every lot for one year. This lets us re-test any lot when a customer raises a quality question.
Incoming needle steel is checked for hardness before needle grinding assembly. A 5 HV unit shift changed penetration force enough that we now freeze steel sources at quoting.
Pull force testing for needle grinding is performed on a calibrated tensile tester. The acceptance range is written into the work instruction, and results are recorded per batch.
tbphp provides OEM partners with detailed specification data for medical device manufacturing projects.
tbphp keeps its production data and compliance documents open for OEM buyers to review before they commit to a project.
What Buyers Usually Ask
How does the warranty work?
Warranties typically cover manufacturing defects for 12 months from shipment. Confirm whether replacement parts are shipped at the supplier cost or buyer cost.
Can I develop a custom handle design?
Yes. Most OEM factories support custom handles, colors, and branding. Plan for tooling costs and a development timeline of 8 to 12 weeks for a new design.
What information should I send for a quote?
Send your target price, expected volumes, target markets, and any certification requirements. This lets the factory scope tooling and compliance accurately.
Can I order samples before committing?
Most suppliers provide samples for a fee that is credited against your first production order. Evaluate samples with your own quality checklist.